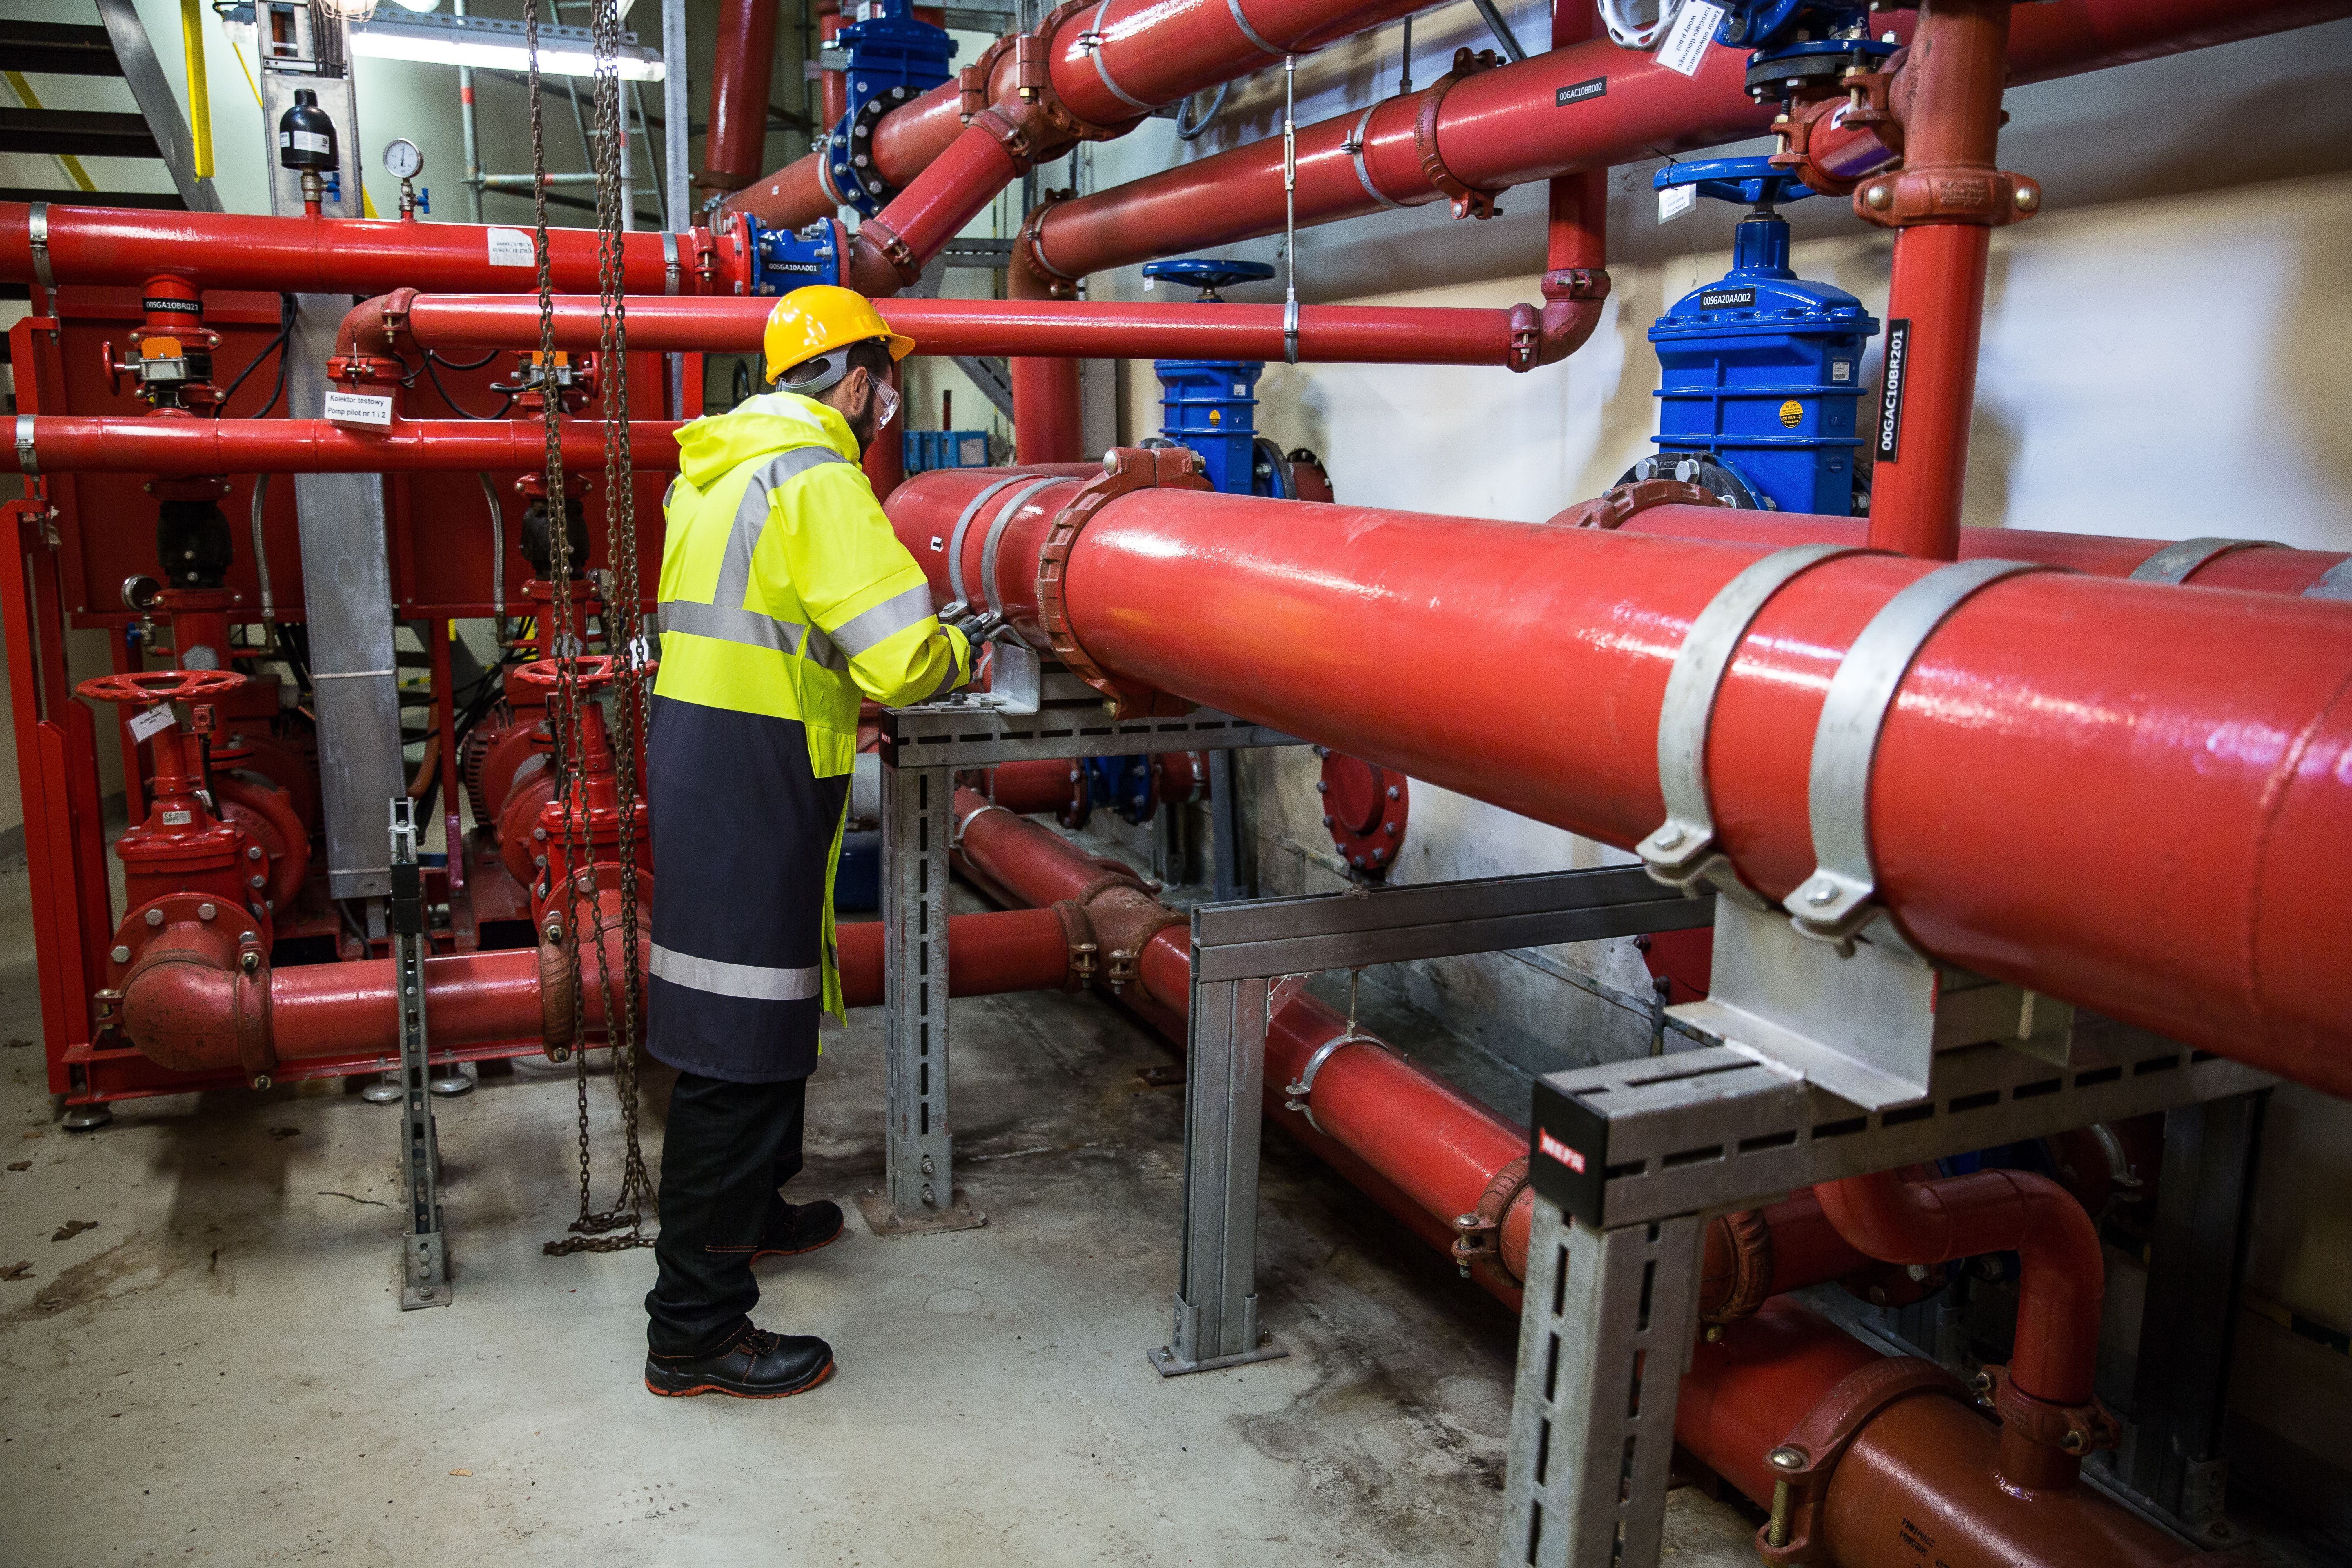
Proven Track Record

Past Completed Projects & Case Studies

Explore our history of executing complex engineering challenges, offshore asset revamps, subsea pipeline repairs, and large-scale terminal overhauls safely, on schedule, and under budget.

Engineering Excellence Across the Energy Value Chain

Over the past two decades, Avenora Energy Solutions has partnered with major national and international oil companies (NOCs/IOCs) to deliver mission-critical field services. Below are detailed operational breakdowns of selected capital projects completed by our engineering and field crew divisions.

Project 1 - Deepwater Riser & Subsea Manifold Integration
Offshore Exploration Location: Gulf Coast Offshore • Duration: 14 Months

Project Delta-7: Deepwater Riser & Subsea Manifold Integration

Executive Summary & Objective: Project Delta-7 involved the complete structural refurbishment, pressure testing, and subsea integration of a 12-slot seabed manifold and high-pressure riser system operating at depths exceeding 4,200 feet. The primary operator faced aging wellhead interfaces and micro-fissure degradation along the secondary manifold headers. Avenora Energy Solutions was contracted as the lead mechanical contractor to execute an emergency turn-around project designed to restore total volumetric throughput without interrupting production on adjacent subsea tie-backs.

Technical Execution & Engineering Challenges: The project scope required an intensive multi-stage execution plan. Our engineering team deployed specialized remotely operated vehicles (ROVs) equipped with ultrasonic wall-thickness sensors to conduct a full structural baseline scan across 18,000 feet of subsea piping. Following diagnostic validation, field crews performed subsea hyperbaric tie-in welding to replace deteriorated flowlines. To handle extreme working pressures up to 12,500 PSI, Avenora designed custom high-nickel alloy sleeve reinforcements, which were lowered and locked into position using specialized heavy-rigging crane barges.

HSE, Compliance & Environmental Controls: Due to harsh offshore marine conditions, safety and environmental protection were paramount. Avenora enforced a strict Zero-Harm containment policy. Zero fluid leakage occurred throughout the 14-month project duration. All weld procedures met API 1104 and ASME Section IX standards, with 100% volumetric non-destructive examination (NDE) applied via automated phased array ultrasonic testing (PAUT). Environmental monitors verified zero disturbance to localized benthic marine habitats during anchor placement and subsea trenching.

Project Outcomes & Value Delivered: Project Delta-7 was delivered 18 days ahead of schedule and 4% under budget. The rehabilitated manifold and riser system restored production capacity to 85,000 barrels of oil equivalent per day (BOED), extending the operational lifespan of the field by an estimated 15 years. The operator awarded Avenora a multi-year master service agreement (MSA) for ongoing subsea maintenance following the success of this project.
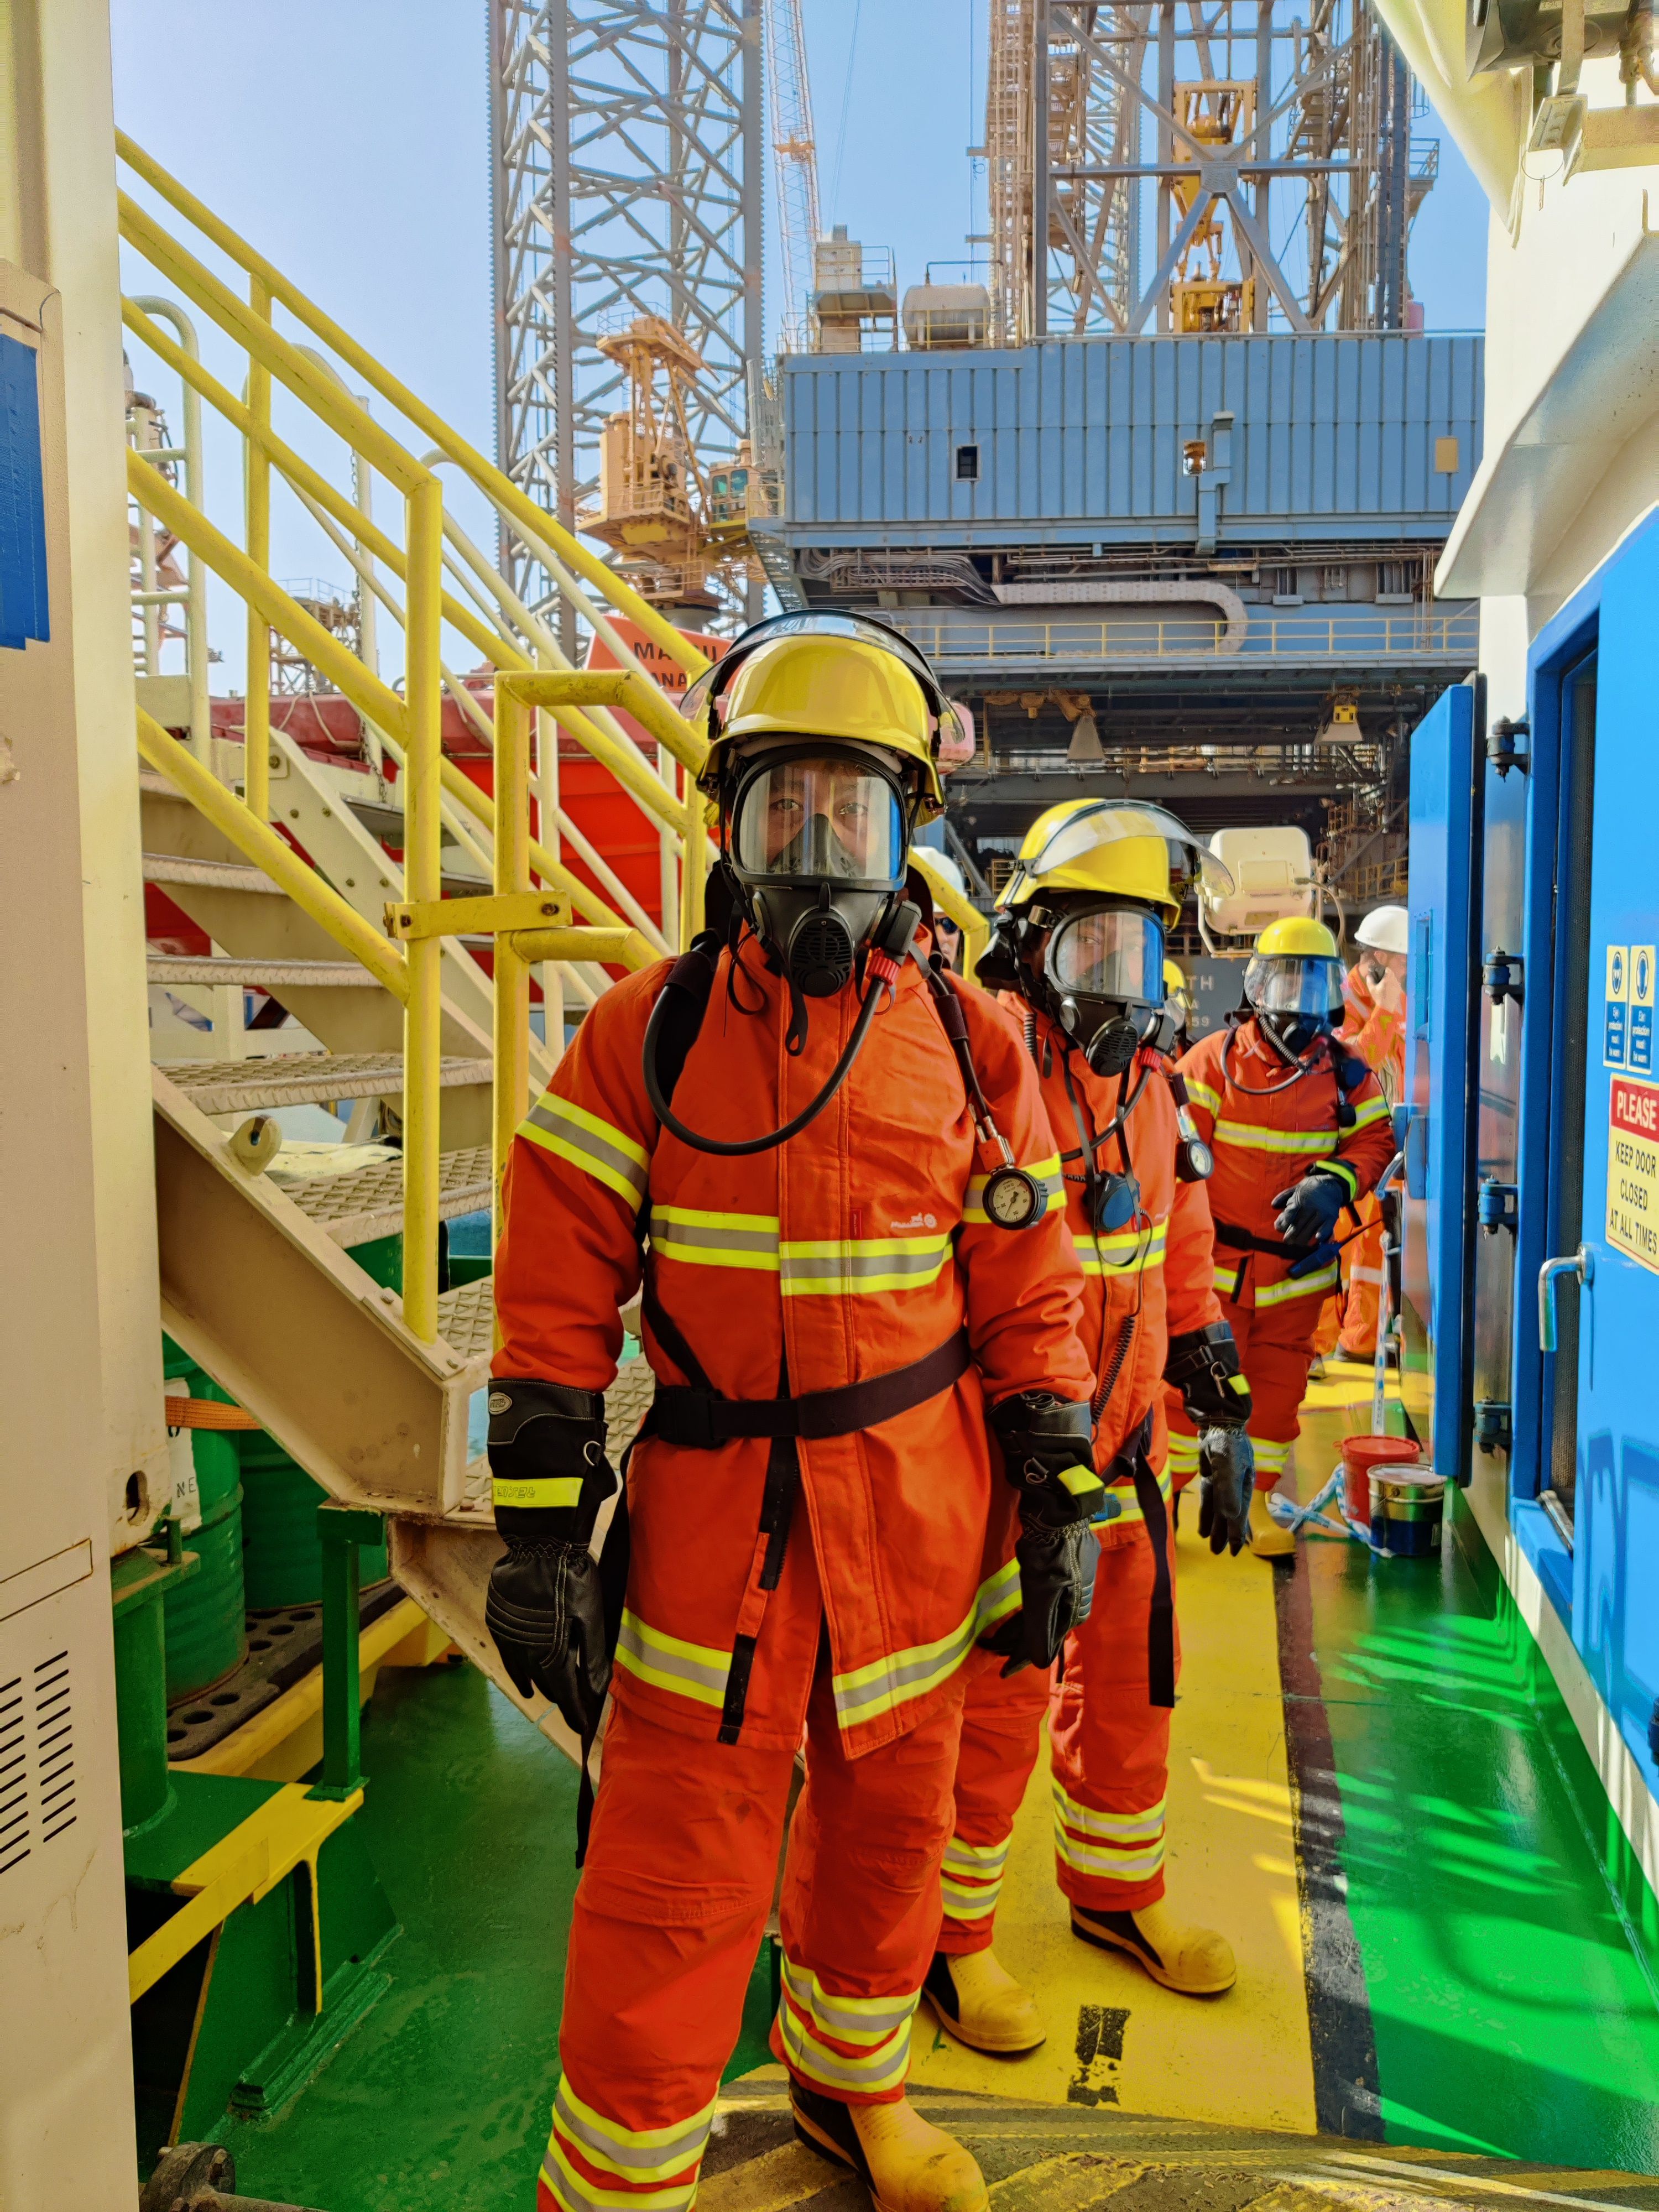
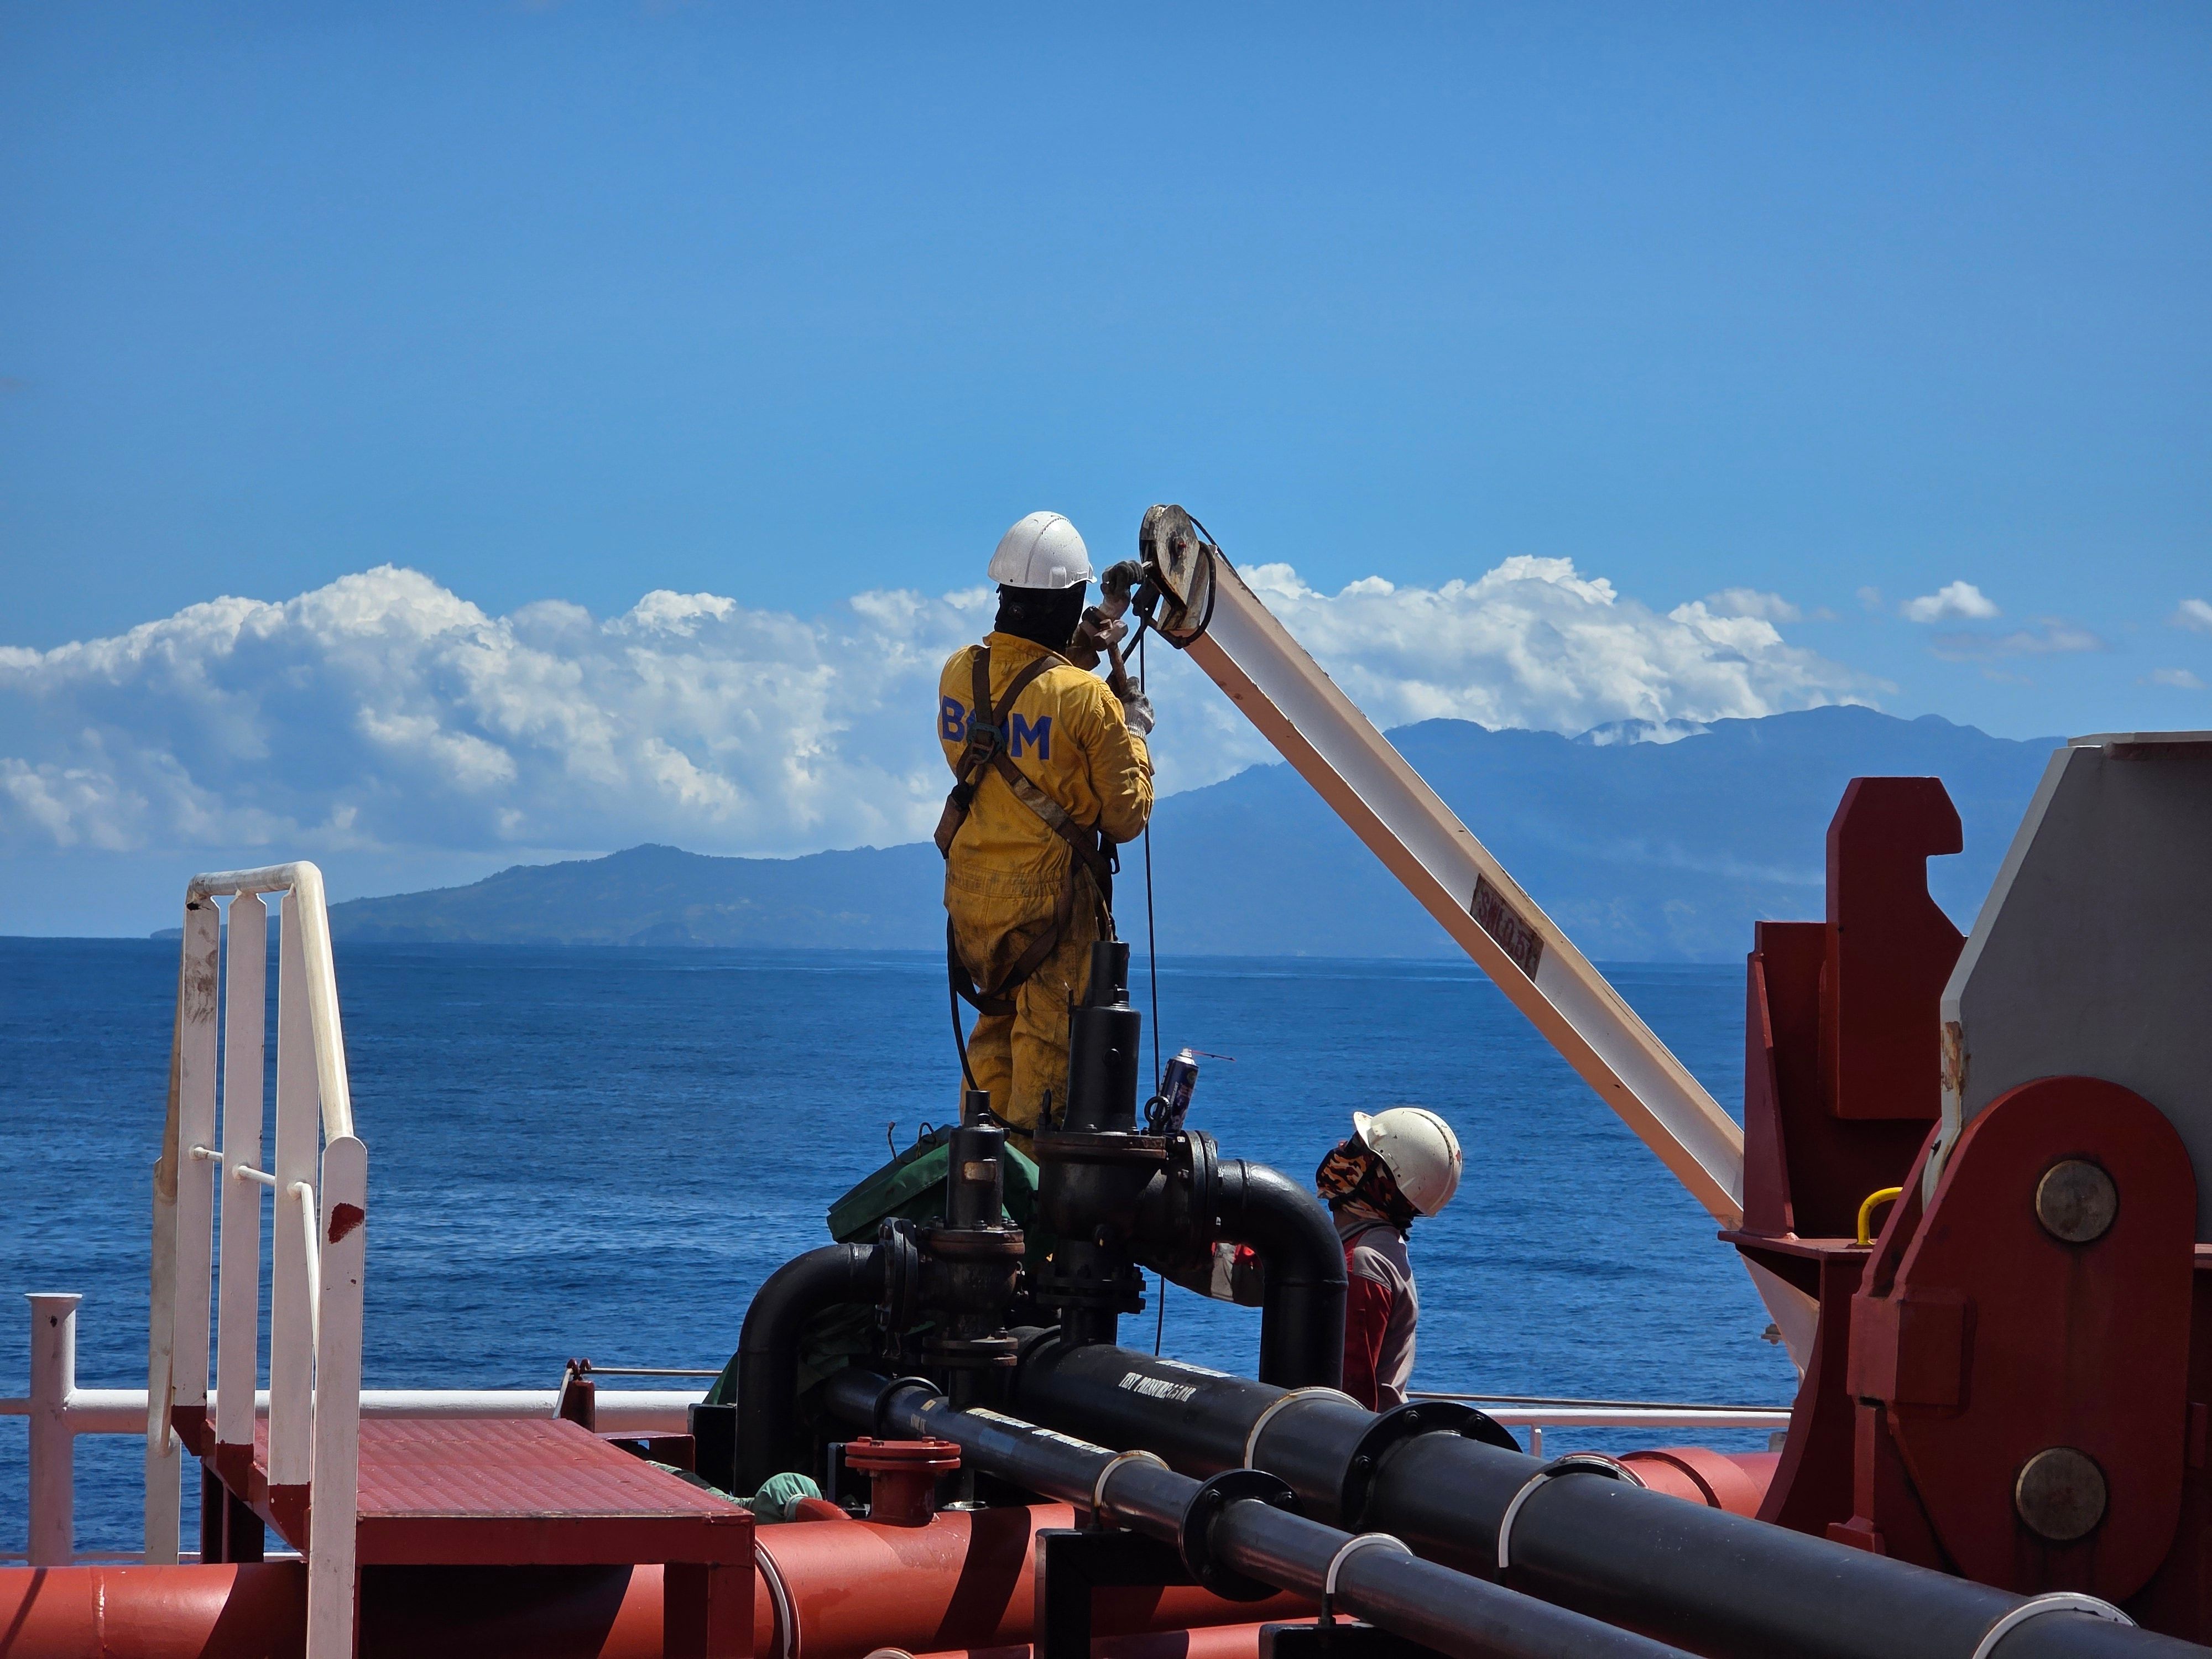
Project 2 - High-Risk Heavy Lift & Platform Topside Overhaul
Offshore Topside Maintenance Location: North Sea Sector • Duration: 8 Months

Project Titan: Offshore Topside Heavy Lift & Rigging Operations

Executive Summary & Objective: Project Titan focused on the removal, overhaul, and re-installation of heavy compression modules located on an aging offshore production platform. Operating in high-energy sea states, the client required a complete structural upgrade of their platform's primary power generation skid and production separation units. The module weights exceeded 320 metric tons, requiring precise rigging, heavy-lift coordination, and structural load distribution calculations to prevent platform instability during lifting phases.

Technical Execution & Rigging Engineering: Avenora’s senior rigging specialists engineered a multi-point lift plan utilizing dynamic ballast compensation systems and high-capacity hydraulic strand jacks. Prior to the physical lift, our team constructed 3D digital-twin simulations to model wind shear, deck load limits, and center-of-gravity shifts during rotation. Over a 45-day continuous operational window, our field crew decommissioned the legacy separation vessels, cut structural tie-downs, and maneuvered the replacement compressor skids into position with sub-millimeter placement accuracy.

Rigorous Quality Control & Risk Mitigation: Working at height in maritime conditions presented extreme safety hazards. Avenora implemented full fall-arrest systems, continuous gas monitoring, and dynamic risk assessments before every shift change. Mechanical piping connections were hot-bolted and flange-tested using hydraulic torque units to eliminate hydrocarbon leak paths. All structural welding passed 100% magnetic particle testing (MPT) and radiographic inspection.

Project Outcomes & Impact: The topside overhaul restored full operating pressure to the platform’s gas-lift operations, increasing daily gas production by 22%. The project achieved over 250,000 man-hours without a single lost-time incident (LTI). The client praised Avenora's rigging team for seamless co-operation with the platform’s live production operations.

Project 3 - Cross-Country Overland Pipeline Replacement
Midstream Logistics Location: Permian Basin Corridor • Duration: 11 Months

Project Apex: Overland Crude Transport Pipeline Modernization

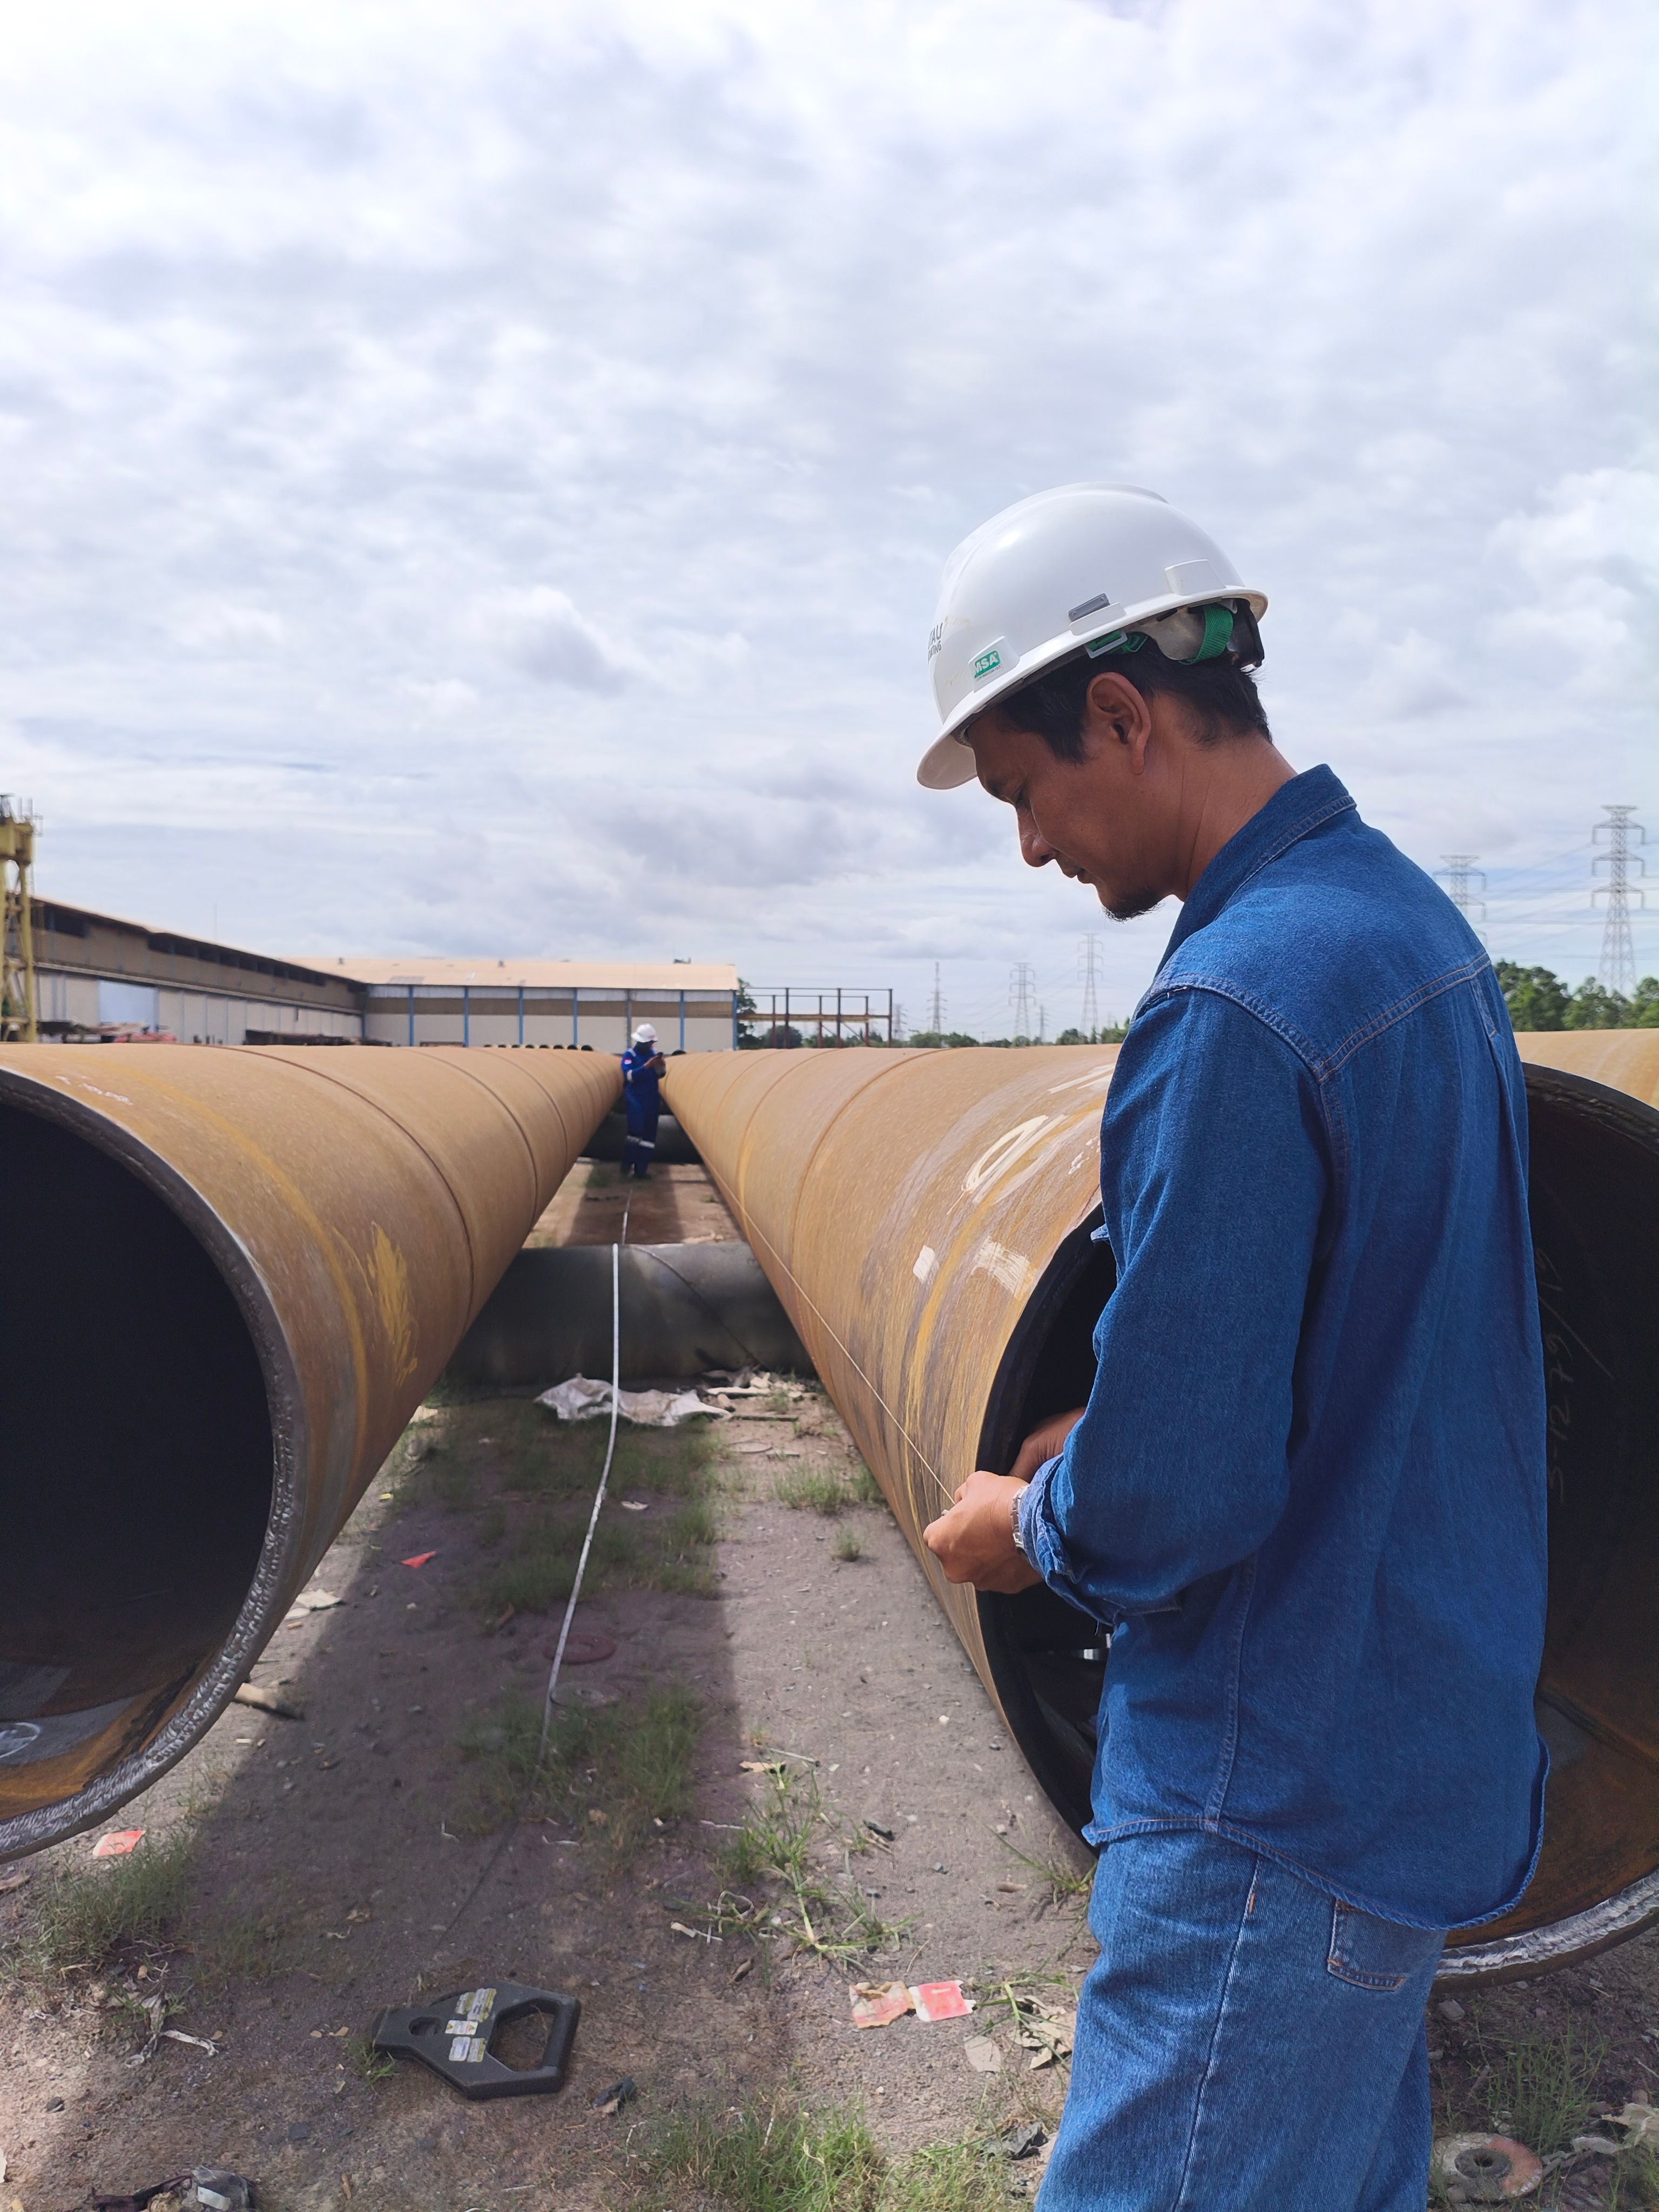
Executive Summary & Objective: Project Apex targeted the replacement and capacity expansion of a 42-mile section of crude oil trunkline traversing challenging terrain and river crossings. The original 24-inch pipeline had operated for over three decades, exhibiting wall thinning due to internal erosion and external soil corrosion. Avenora Energy Solutions was tasked with installing a modern 36-inch API 5L X70 high-yield steel pipeline alongside the existing right-of-way without interrupting crude supply to regional refineries.

Civil & Mechanical Construction Execution: Construction teams managed clearing, trenching, pipe bending, field welding, and backfilling operations across diverse geological formations. To cross two major water bodies, Avenora utilized Horizontal Directional Drilling (HDD) to bore under riverbeds at depths up to 60 feet, pulling pre-welded pipeline strings without disturbing aquatic ecosystems. Our certified welding crews performed over 3,200 manual and automated girth welds, using high-performance fusion-bonded epoxy (FBE) coatings to protect every joint.

Regulatory Integrity & Testing Protocols: Upon completion of pipe laying, Avenora conducted comprehensive hydrostatic testing, pressurizing section segments to 1.5 times the maximum allowable operating pressure (MAOP) for 24 continuous hours. Magnetic flux leakage (MFL) smart pigs were launched to verify pipe roundness and coating integrity. Environmental restoration teams re-contoured the topsoil and re-seeded native vegetation along the right-of-way to meet federal land compliance requirements.

Project Outcomes & Key Milestones: The upgraded trunkline increased crude transport capacity by 65%, reaching 450,000 barrels per day. By employing HDD methods, Avenora saved the operator approximately $3.2M in conventional bridging infrastructure while achieving zero environmental citations throughout construction.

Project 4 - Trench Pipe Welding
Pipeline Rehabilitation Location: Coastal Marshes • Duration: 6 Months

Project Trench-Guard: In-Service Pipeline Sleeve Repair

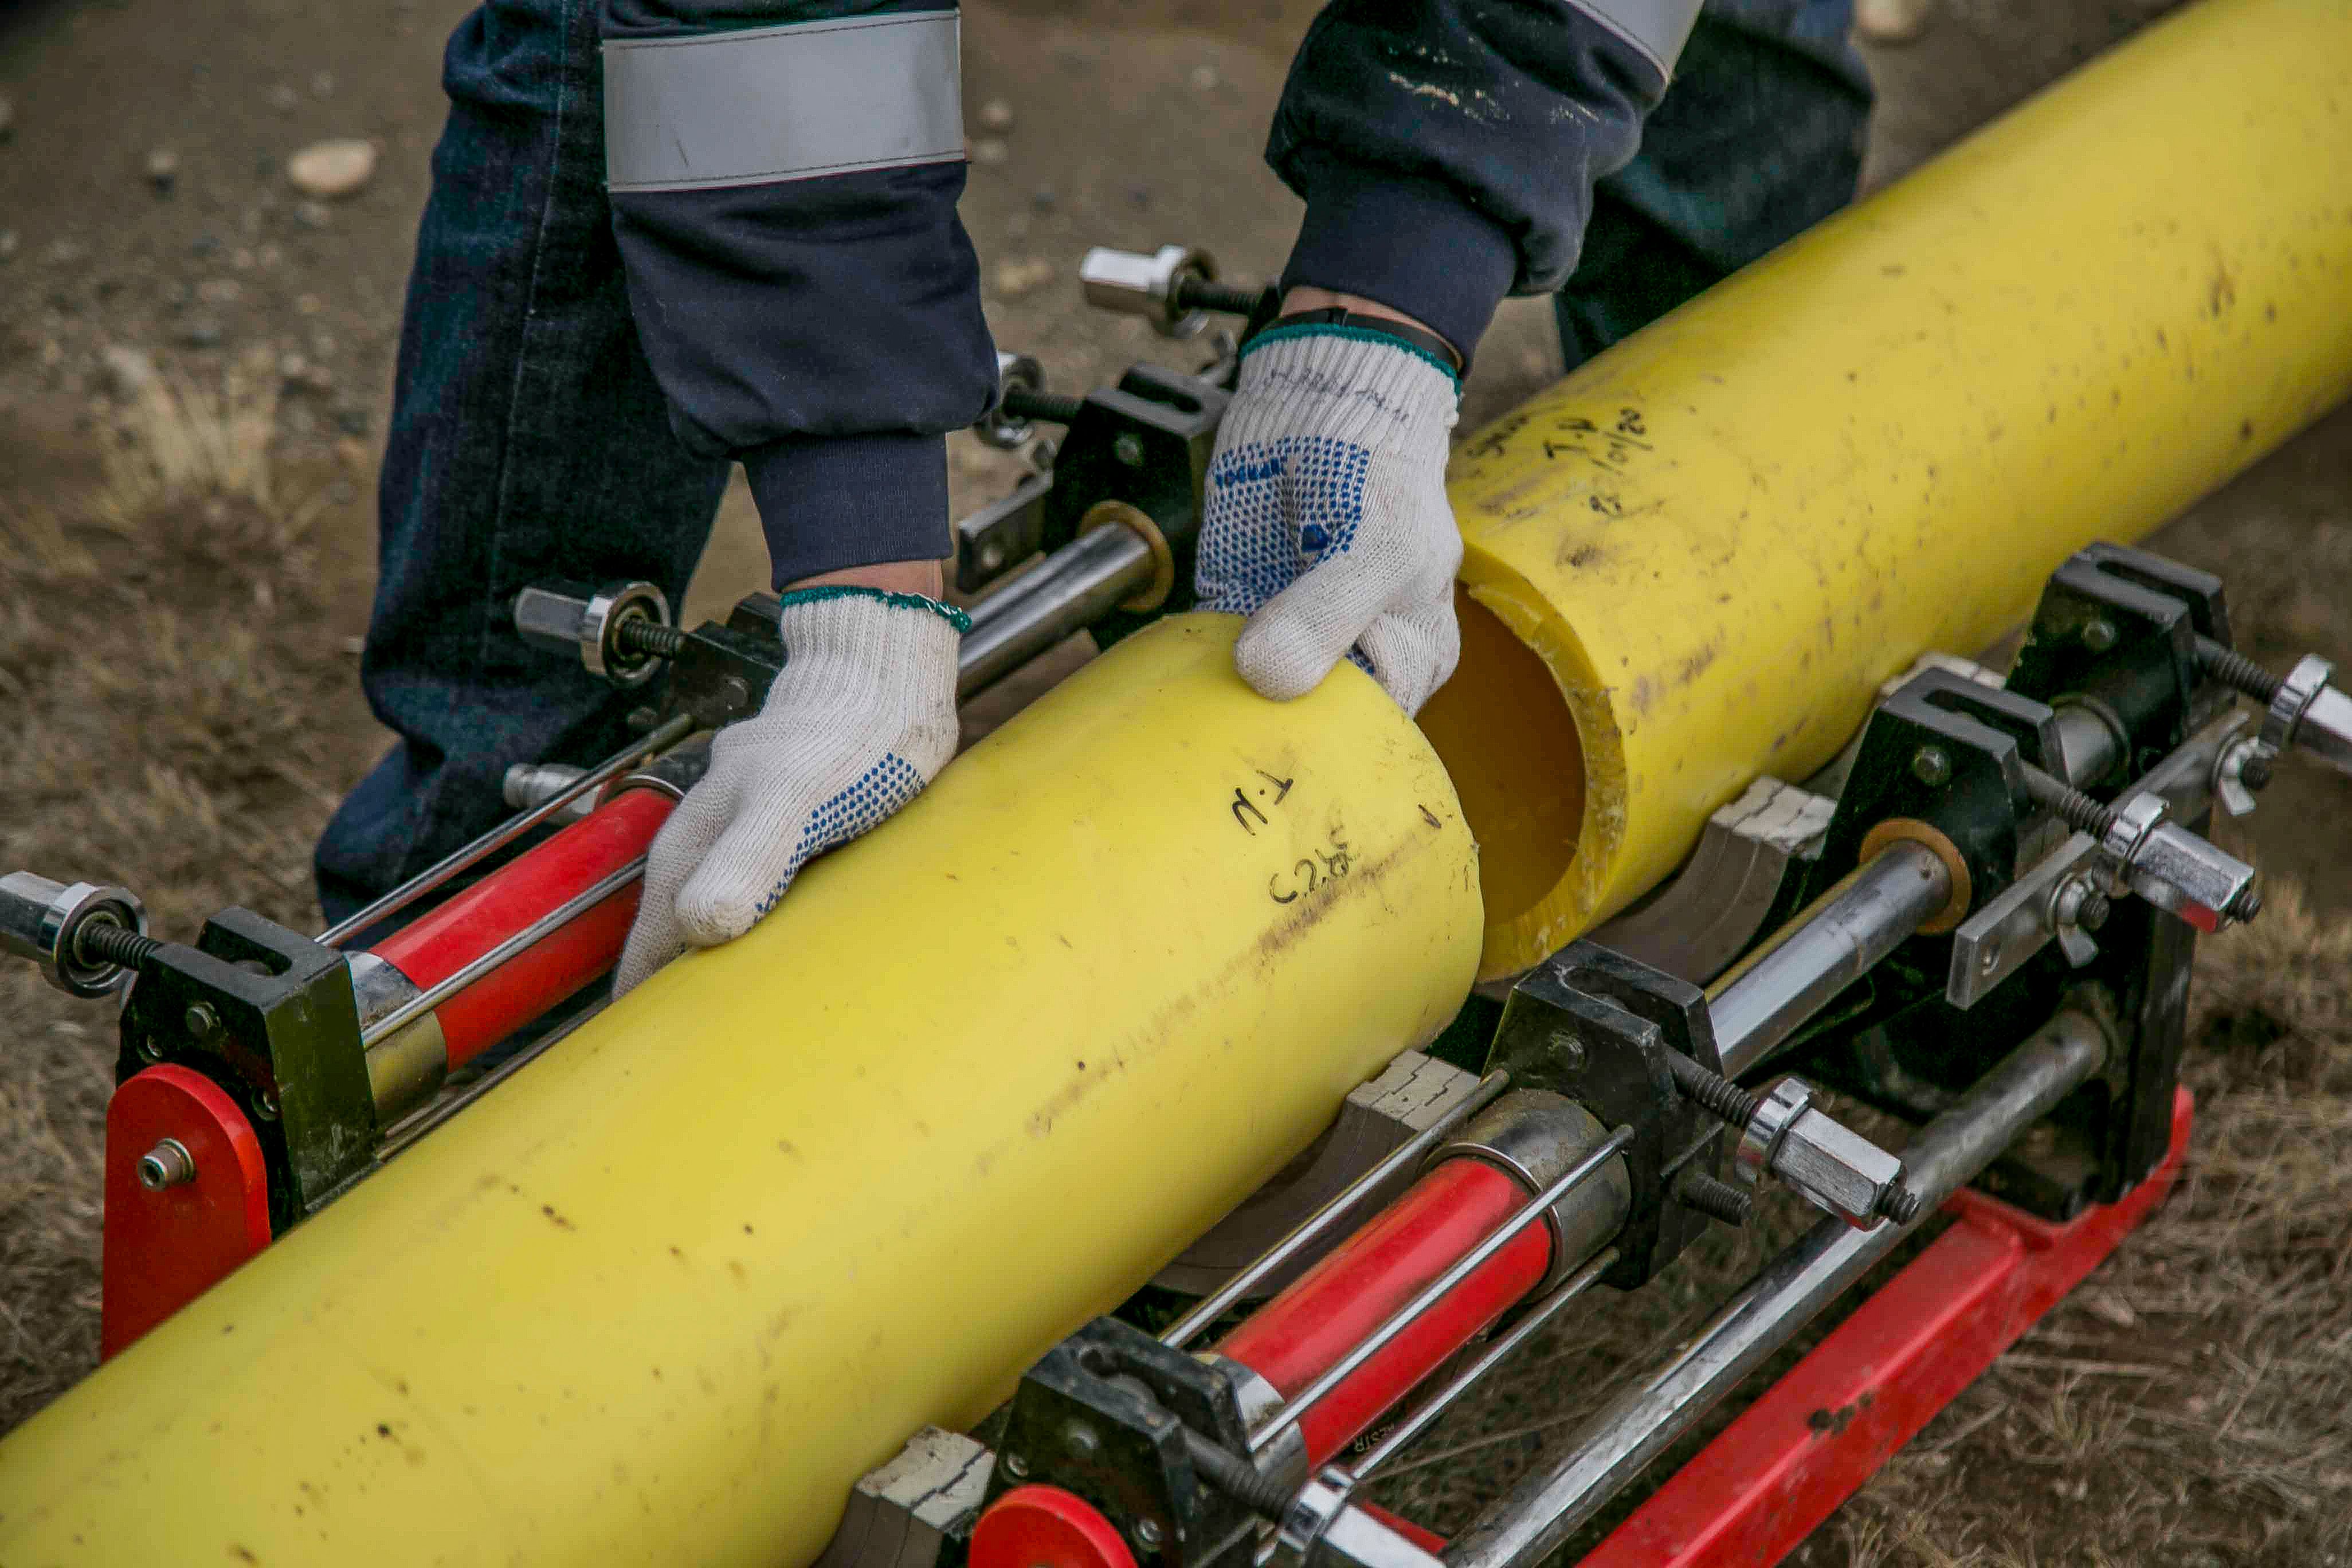
Executive Summary & Objective: Project Trench-Guard presented a highly specialized engineering challenge: repairing localized wall-loss anomalies on a live, high-pressure natural gas transmission line without shutting down gas flow to a major metropolitan power grid. The line was submerged in a wet, marshy environment, requiring temporary shoring, water dewatering, and specialized hot-tap welding techniques on active, pressurized piping.

Engineering & Execution Methodology: Avenora deployed specialized trench shoring boxes and continuous pumping systems to create safe, dry working cells around seven compromised pipe sections. Our high-pressure welding specialists used low-hydrogen electrode techniques to install full-encirclement Type B steel pressure sleeves over damaged pipe segments. Pre-heat and interpass temperature controls were continuously monitored with infrared sensors to eliminate hydrogen cracking risks associated with cooling effects from internal gas flow.

Safety & Real-Time Monitoring: Working inside confined trench environments on live gas lines required real-time gas monitoring, continuous fresh-air blowers, and dedicated safety watch personnel. Acoustic emission monitoring was applied during the welding process to detect micro-strains or structural shifts in real time.

Project Outcomes: All seven damaged segments were fully encased and structural integrity was restored to 100% operating specification. The project was completed without interrupting gas service to over 1.2 million end users, saving the client an estimated $12M in potential downtime penalties.

Project 5 - Refinery Processing Units
Downstream Processing Location: Industrial Refining Hub • Duration: 18 Months

Project Vulcan: Refinery Fluid Catalytic Cracking Unit (FCCU) Turnaround

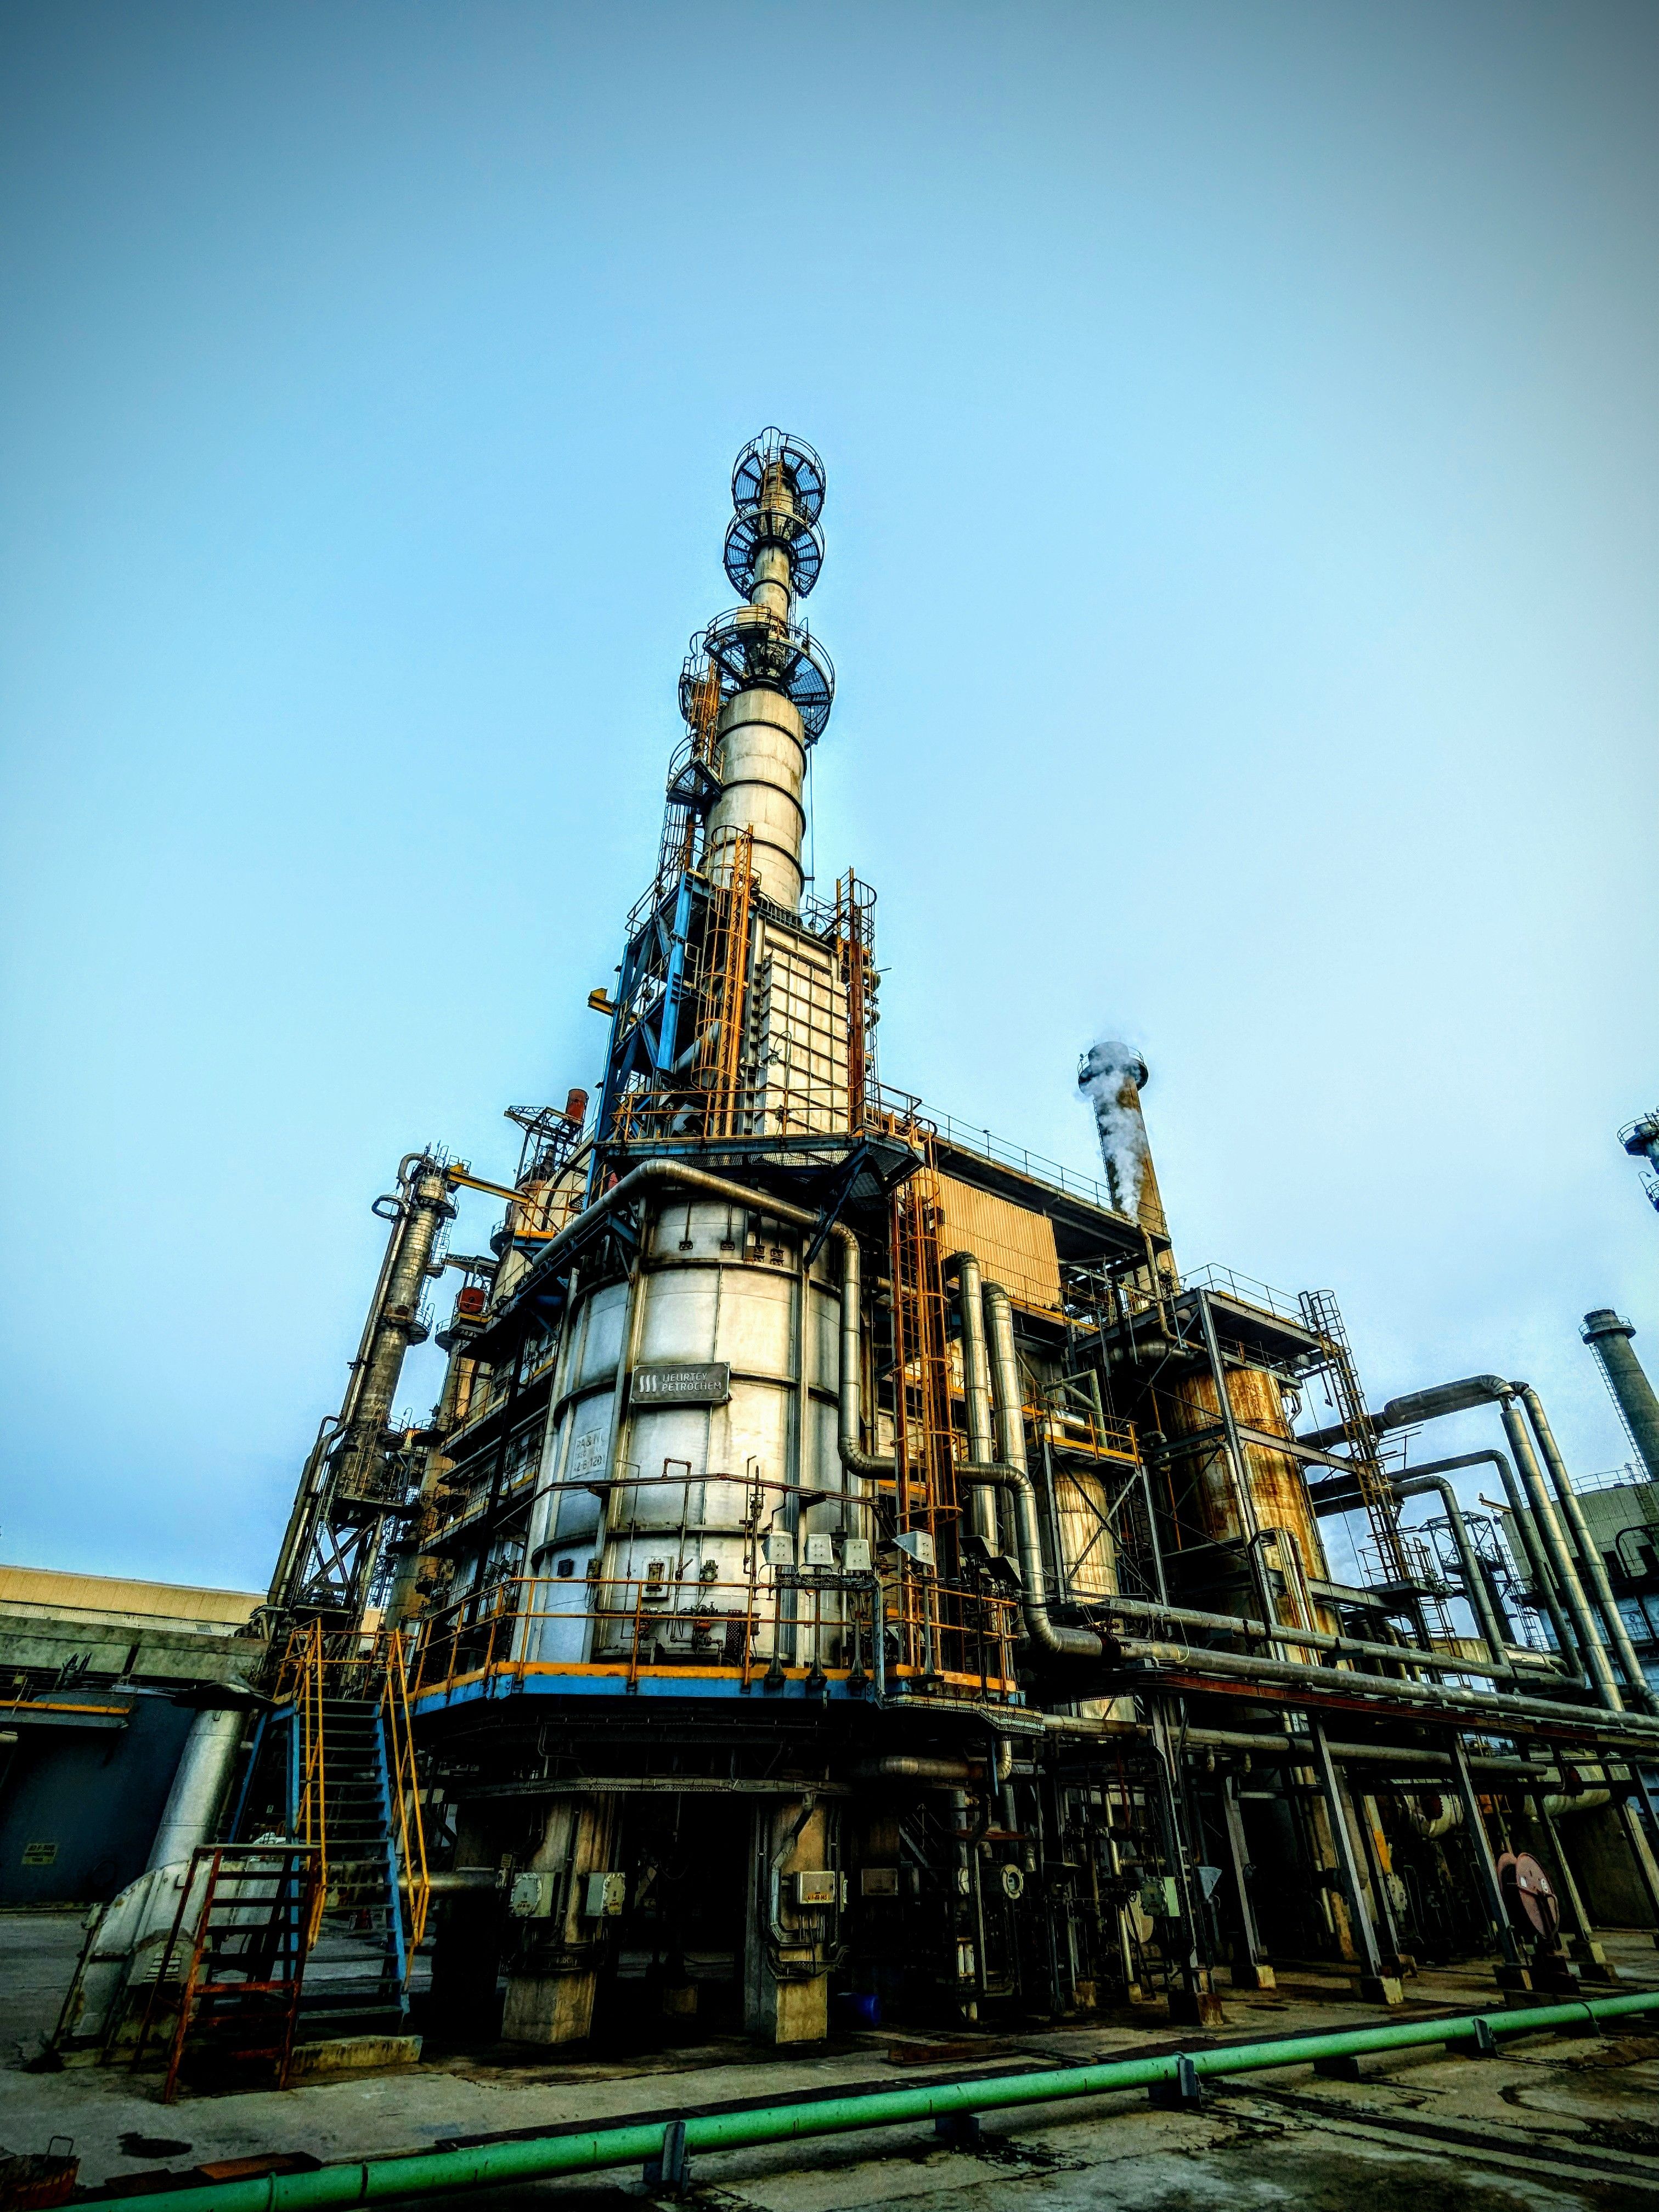
Executive Summary & Objective: Project Vulcan comprised a major turnaround and revamping of a primary Fluid Catalytic Cracking Unit (FCCU) and downstream fractionation column at a major petroleum refinery. The plant owner aimed to improve yield efficiency for ultra-low sulfur diesel (ULSD) while replacing heavily coked heat exchanger bundles, high-temperature piping, and pressure relief valves.

Mechanical & Piping Engineering: Over 450 skilled craft personnel were deployed under Avenora’s supervision during a scheduled 45-day refinery shutdown window. The team dismantled, decontaminated, and replaced 14,000 linear feet of high-alloy process piping, installed upgraded hydro-processing control valves, and refurbished internal column trays. Hydro-jetting teams cleared internal scaling across heat exchangers, restoring thermal transfer performance.

Quality Assurance & Plant Re-Commissioning: Strict QA/QC protocols were enforced throughout the turnaround. Every flange assembly was verified using digital torque logging, and positive material identification (PMI) testing was conducted on all newly installed alloy fittings. Pressure vessel hydro-testing was executed in accordance with ASME Section VIII regulations prior to plant re-pressurization.

Project Outcomes: The refinery successfully restarted operations 3 days ahead of schedule. The modernized FCCU achieved a 14% increase in ULSD yield while reducing energy consumption by 8%, significantly lowering operational emissions for the facility.

Project 6 - Offshore Platform Derrick
Offshore Drilling Integrity Location: Deepwater Basin • Duration: 5 Months

Project Sentinel: Offshore Derrick Refurbishment & Structural Bolstering

Executive Summary & Objective: Located 80 miles offshore, Project Sentinel focused on structural maintenance, crown block re-alignment, and derrick reinforcement for a fixed deepwater drilling platform. Saltwater exposure and high wind loads had induced surface oxidation and structural fatigue along the upper derrick framing, necessitating structural steel replacement and recoating.

Rope Access Engineering & Execution: To avoid costly scaffolding installation over water, Avenora utilized SPRAT/IRATA certified industrial rope access technicians. Teams ascended the 180-foot derrick structure to conduct ultrasonic thickness testing, remove compromised structural gusset plates, and weld replacement high-strength structural members into place. High-durability marine epoxy coating systems were applied to protect against environmental degradation.

Safety Controls & Uninterrupted Operations: Operations were coordinated around ongoing platform drilling schedules. Dropped-object prevention protocols were rigorously enforced, utilizing tool lanyards and safety netting systems. The project logged over 40,000 rope-access work hours without incident.

Project Outcomes: Structural integrity certification was renewed for an additional 10 years of heavy drilling service. The operator avoided over $4M in downtime costs by utilizing Avenora's rope access methodology instead of conventional scaffolding platforms.

Project 7 - Storage Tank Terminal Expansion
Storage & Terminal Assets Location: Deepwater Port Terminal • Duration: 16 Months

Project Harbor-Tank: Storage Terminal Expansion & API 653 Upgrades

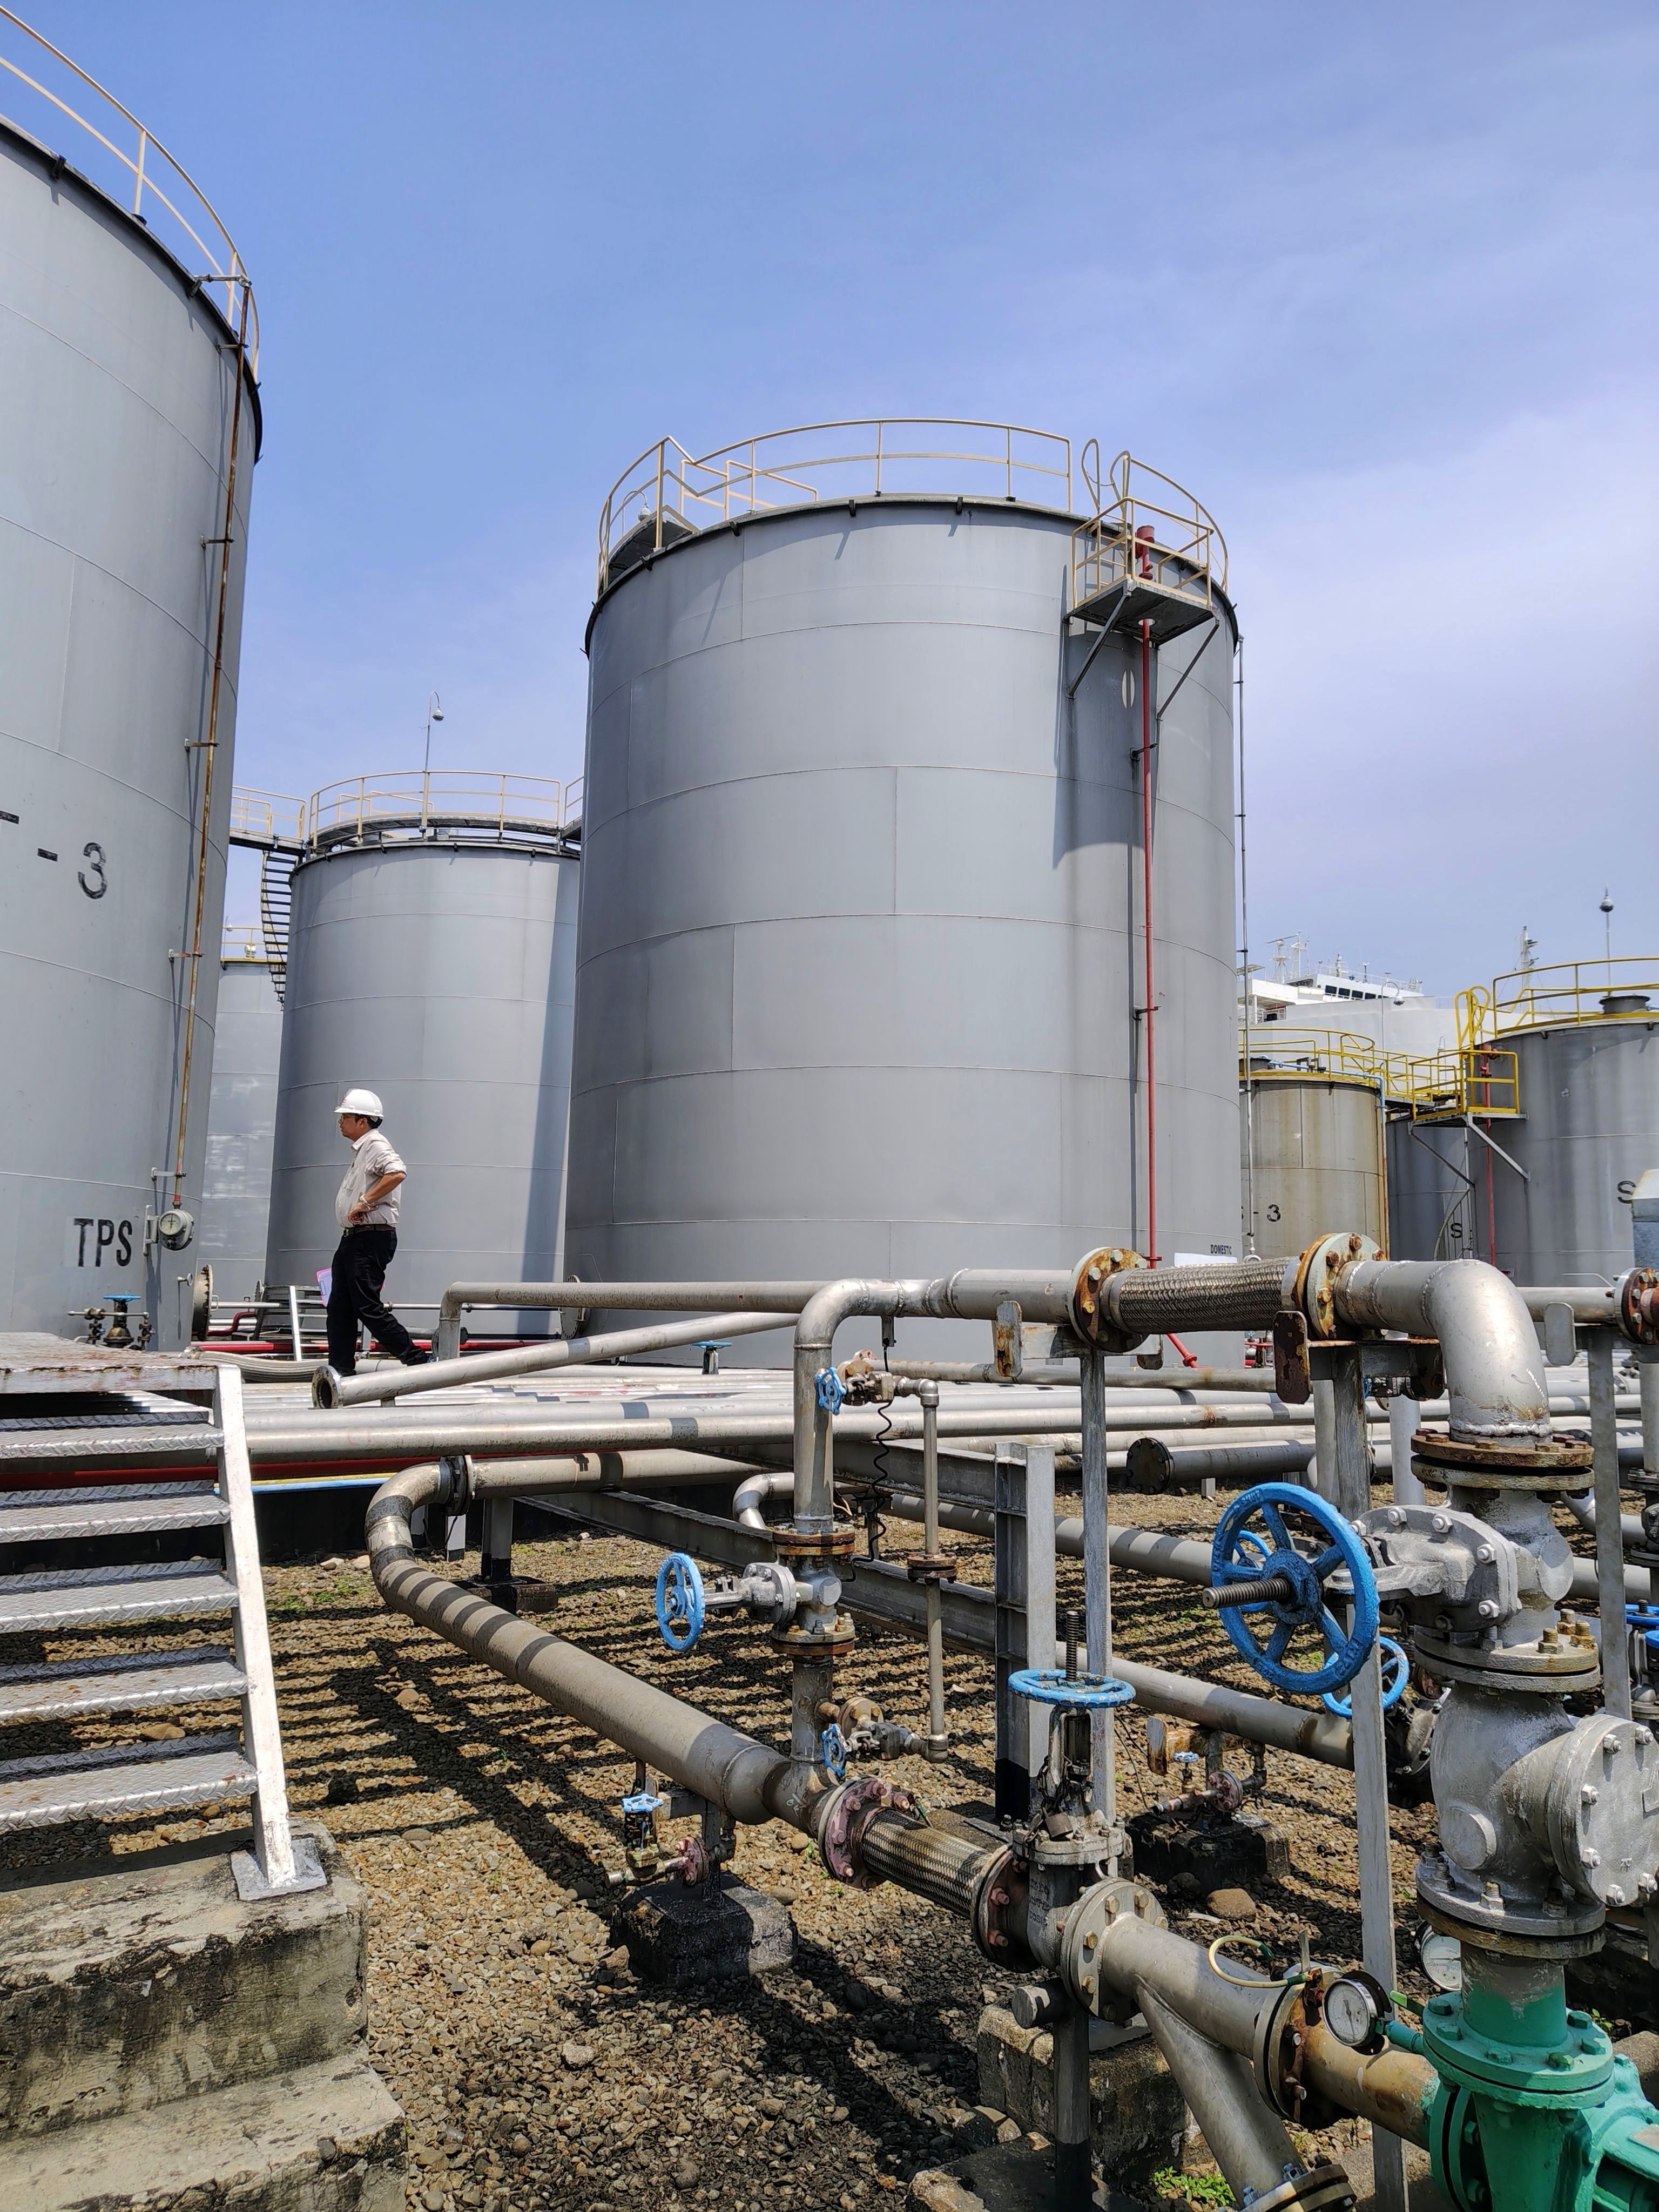
Executive Summary & Objective: Project Harbor-Tank encompassed the construction of four new 250,000-barrel floating-roof storage tanks and the complete mechanical overhaul of eight existing API 650 storage tanks at a marine export terminal. The project aimed to double terminal storage capacity while bringing older assets into full compliance with updated environmental secondary containment rules.

Civil, Tank Shell & Foundation Engineering: Avenora managed civil site prep, pile driving, ring-wall foundation installation, and tank plate erection. Automatic girth welders were used for shell plate joining, followed by vacuum box testing on all floor seams and double-pigment leak testing on internal floating roofs. Secondary containment dikes were reinforced with impermeable geotextile liners and concrete retaining walls.

Terminal Piping & Automated Transfer Systems: In addition to tank construction, Avenora installed 8,500 feet of 24-inch manifold piping, automated motor-operated valves (MOVs), and fiscal metering skids to support rapid vessel loading operations.

Project Outcomes: The expanded terminal successfully increased total storage capacity by 1 million barrels, enabling the facility to service larger Suezmax crude carriers. The project was completed on schedule with zero regulatory non-compliances.

Project 8 - Petrochemical Facility Aerial View
Petrochemical Infrastructure Location: Gulf Coast Industrial Zone • Duration: 24 Months

Project Synergy: Petrochemical Piping & Distillation Unit EPC Support

Executive Summary & Objective: Project Synergy was a multi-year engineering, procurement, and construction support effort focused on integrating a new ethylene cracker unit into an active petrochemical complex. Avenora Energy Solutions served as the specialized piping and mechanical tie-in contractor responsible for connecting new processing towers to existing utility grids and steam supply lines.

Complex Field Integration & Hot Tapping: The project required over 50 complex hot taps and line stops on operational steam and chemical headers, preventing plant-wide shutdowns. Avenora engineered custom high-temperature split-tees and deployed specialized tapping machines capable of drilling into lines operating at 650°F and 800 PSI.

Digital Quality Control & Asset Handover: Avenora implemented full digital tracking for every weld, bolt torque, and NDE report via a centralized BIM model. Over 5,000 isometric drawings were executed, inspected, and turned over to the client with zero punch-list delays.

Project Outcomes: Project Synergy achieved successful commissioning with 100% first-pass weld compliance. The new facility expansion increased high-density polyethylene production by 400,000 metric tons per year, meeting growing regional demand.

Have an Upcoming Capital Project or Turnaround?

Put Avenora's proven engineering track record to work on your next onshore or offshore asset maintenance scope.

Work With Our Project Team